If you’ve ever stood by a lathe and watched a chunk of copper bar transform into a clean, precise part, you know that turning isn’t just about skill—it’s about working with a material that behaves as unpredictably as it does reliably. As a copper turning supplier, I get asked this question at least once a week: “What hardness of copper is actually best for turning?” It’s not a yes-or-no answer, and if you’ve ever grabbed a soft, annealed copper billet only to spend 45 minutes fighting with stringy swarf that clogs your tool, you know exactly why that matters. Hardness is the sweet spot that separates a scrap pile from a high-quality machined component, and over the past 12 years in this trade, I’ve learned to read that number like a road map—one that leads to smooth cuts, longer tool life, and parts that fit exactly as they should. Copper Turning
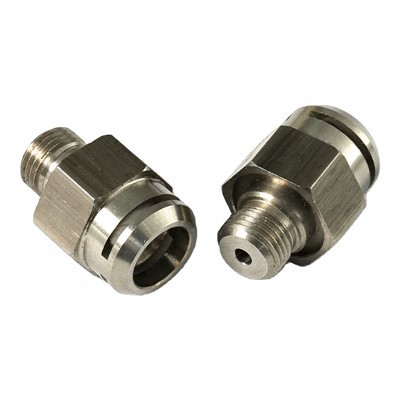
First, let’s get one thing straight: copper isn’t a single material. It’s a family. Pure copper (often called electrolytic tough pitch, or ETP copper, for its 99.9% purity) is the most common stock we work with for turning, because it’s highly conductive and ductile—perfect for electrical connectors, bus bars, and plumbing fittings. But when that pure copper is annealed (heated and slow-cooled to soften it), its hardness drops to around 35 to 45 HV (Vickers hardness). That sounds low, but here’s the catch: annealed ETP is so soft that when you run a lathe tool across it, the material doesn’t shear cleanly—it smears. It pulls off in long, tangled swarf that wraps around your workpiece, scores the surface, and can even break your tool tip if you don’t catch it fast. I remember my first year in the trade, a customer brought in annealed copper rod and asked us to turn 500 precision pins. We ran it at standard turning speeds, and by the end of the shift, we’d broken three carbide inserts and had to rework 120 parts because of smeared burrs. We switched to harder, half-hard copper and cut the rework rate to zero, and that’s when I realized hardness isn’t just a number—it’s a productivity tool.
So what’s the sweet spot for turning? After testing hundreds of batches, collaborating with metallurgists, and fixing more bad jobs than I can count, I’ve found that copper with a hardness range of 60 to 100 HV is where most turning operations thrive. Wait—let’s break that down. Below 60 HV, you’re dealing with either fully annealed pure copper or very low-alloy copper that’s too soft. Above 100 HV, you get into harder copper alloys like C17200 beryllium copper, which is great for springs and electrical contacts, but that extra hardness makes it abrasive. It wears tools faster, and while it can be turned, it requires much slower speeds and special tooling that most job shops don’t keep on hand. The 60–100 HV range hits the middle: it’s hard enough to shear cleanly when cut, but still ductile enough to avoid being too abrasive, so tools stay sharp and swarf breaks into small, manageable chips instead of tangling.
Let’s talk about how copper reaches that hardness, because it’s not just about the material itself—its processing matters. Copper gets harder in two main ways: annealing (softening) and cold working (strain hardening). Half-hard copper, which is the most common in this range, is produced by cold drawing the rod through a die after casting. That pulling process compresses the copper’s crystal structure, making it denser and harder without adding any alloys. Half-hard ETP copper clocks in at around 60 to 80 HV, and that’s the workhorse of copper turning. We use it for everything from small terminal pins to larger plumbing valves, and it machines 30% faster than annealed copper, with 20% longer tool life. It’s also more dimensionally stable, which is critical for tight-tolerance parts—you don’t have to worry about the workpiece warping mid-turn because it’s too soft to hold its shape.
Then there’s the upper end of that range: 80 to 100 HV. That’s where you find high-strength copper alloys, like C11000 copper with slight additions of chromium or zirconium, or even some low-alloy brasses (wait, brass is a copper alloy, too—important not to mix that up with pure copper, though I’ll get to that in a minute). Copper at the 90 HV mark is perfect for turning parts that need extra wear resistance, like gears for small motors or hydraulic fittings that have to seal tightly. I recently worked with a customer making small hydraulic valve stems; they’d been using annealed copper, and the valves were leaking within a month because the soft material deformed under pressure. Switched to 92 HV copper, and the failure rate dropped to less than 1%—game changer. But here’s the caveat: above 100 HV, like with C17200 beryllium copper at 150 HV, turning becomes a different beast. You have to use polycrystalline diamond (PCD) tools instead of carbide, run speeds 50% slower, and even use coolant designed for high-hardness non-ferrous metals. It’s not impossible, but it’s not the same as the 60–100 HV sweet spot most turning operations rely on.
Wait, I mentioned brass—let’s clarify that, because a lot of people mix copper and brass when talking about turning hardness. Brass is an alloy of copper and zinc, and its hardness ranges from around 80 HV for annealed yellow brass to 140 HV for high-leaded free-machining brass like C36000. That free-machining brass is a popular choice for turning because the lead additions make it easy to shear, so swarf breaks well. But it’s not pure copper, and if you’re looking for parts that need high conductivity or corrosion resistance (like electrical components or outdoor plumbing), pure copper in the 60–100 HV range is better. As a copper turning supplier, we make it a point to explain that difference to every customer, because ordering the wrong material isn’t just about machining—it’s about the part’s end use. A customer who needs a conductive terminal won’t be happy with a brass part, no matter how well it turns.
Now, let’s get practical: how do you measure this hardness, and why does it matter for actual turning on the shop floor? Most small machine shops use a portable hardness tester, or they rely on the material supplier’s certification, which is standard for copper bar stock. When we get a batch of half-hard copper, we spot-check every third bar with a Vickers tester to make sure it’s between 65 and 75 HV—sometimes during shipping, a bar can get cold-worked unevenly, throwing off the hardness. If the hardness is off, we’ll run a test turn on a sample: if the swarf is stringy and the surface finish is rough, we know it’s too soft, and we’ll either anneal it slightly (a quick oven cycle brings it down 5–10 HV) or request a replacement batch. If it’s too hard, like over 100 HV, we’ll suggest stress-relieving it, which is heating it to 150–200°C for an hour to take the edge off—no need for a full anneal, which would make it too soft.
I’ve seen too many shops waste money by ignoring this. Last year, a small job shop called us upset because they’d bought a cheap batch of copper, turned 2,000 parts, and half were defective. When we tested their stock, it was annealed copper at 38 HV—way too soft for turning. They’d saved 10 cents a pound on the bar stock, but they spent $1,200 reworking parts and $800 on new tooling, for a net loss of over $2,000. That’s the kind of mistake that makes me want to grab a lathe and show them exactly how hardness impacts each cut. At the end of the day, the right hardness isn’t just a technical spec—it’s a cost saver.
Let’s also talk about exceptions, because no rule is universal. For example, very large copper parts, like those for electrical bus ducts, can be turned from softer copper (around 50 HV) because they’re thicker and don’t require tight surface finishes. The hardness there matters less because the part isn’t subject to the same machining stresses as small, precision parts. Or if you’re doing rough turning, you can work with slightly softer copper, as long as you follow up with a finish cut on harder stock. But 9 times out of 10, for most copper turning operations—precision pins, terminals, valves, fittings—sticking to 60–100 HV will give you the best results.
Another point: tool life is directly tied to copper hardness. Carbide inserts, the most common tool for turning copper, last 2–3 times longer on 70 HV half-hard copper than on annealed 35 HV copper. Why? Because soft copper smears across the tool’s edge, building up a built-up edge (BUE) that changes the tool’s geometry, leading to rough cuts and faster wear. Harder copper shears cleanly, so there’s almost no BUE, and the tool edge stays sharp longer. I’ve run the same carbide insert on 70 HV copper for 400 parts, and on annealed copper, it only lasted 150 parts. That’s a huge difference in tooling costs, especially for high-volume jobs.
What about surface finish? If you need a smooth, shiny surface on your turned copper part—say, for a decorative component or a part that will be plated—hardness is key. Soft copper tends to have a rough, uneven surface because of the smeared swarf, while 60–100 HV copper produces a finish that’s within Ra 0.8 to 1.6 micrometers, which is perfect for most applications, and you can even get it down to Ra 0.4 with a polished tool and a light finish cut. I recently delivered a batch of copper clock parts to a customer, and they told me the surface finish was so good, they skipped the polishing step entirely—another cost saved.
Now, let’s address something I hear a lot: “Why not just use the hardest copper you can find?” The answer is simple: functionality. If you have a part that needs to be bent, formed, or shaped after turning, hardness matters. Copper at 60–100 HV is still ductile enough to be bent into a 90-degree angle without cracking, while copper over 120 HV is too brittle for post-machining forming. For example, a copper bracket that gets turned and then bent for a mounting application needs to be in the lower end of that range, around 60–70 HV, while a valve stem that only needs turning and no forming can be in the upper range, 90–100 HV. It’s all about matching the hardness to the part’s end use, which is something every good copper turning supplier will help you figure out.
So, to wrap this up: the hardness of copper suitable for turning isn’t a fixed number—it’s a range, and it depends on what you’re making, how you’re machining it, and what you need the part to do. For most precision turning operations, that sweet spot is 60 to 100 HV, with half-hard ETP copper (60–80 HV) being the most common and versatile choice. It balances machinability, tool life, surface finish, and ductility, so you get parts that are accurate, cost-effective, and fit for their intended purpose.
At the end of the day, I’ve spent 12 years turning copper, and I’ve learned that the best parts don’t come from the fastest machines or the most expensive tooling—they come from paying attention to the material. If you’re working with copper that’s too soft, you’re fighting an uphill battle with swarf and rework. If it’s too hard, you’re wasting money on tooling and slower speeds. But if you land in that 60–100 HV range, the lathe hums, the swarf comes off in small, neat chips, and the parts roll out perfectly every time.
If you’re working on a project and you’re not sure what copper hardness is right for your turning job, or you need consistent, high-quality copper bar stock for your operations, don’t guess. Reach out to discuss your requirements. We’ll talk through your part design, end use, and machining setup, and help you pick the right material and hardness to get the job done right the first time.
CNC Turning References
ASM International. (2019). Copper and Copper Alloys: Properties and Processing. ASM Handbook, Vol. 15: Casting.
Dudzinski, D., et al. (2017). Machining of Non-Ferrous Metals: A Review. Journal of Materials Processing Technology.
Kovacic, M., & Julie, J. (2020). Strain Hardening of Electrolytic Tough Pitch Copper. Materials Science and Engineering: A.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
We’re well-known as one of the leading copper turning manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy customized copper turning made in China here from our factory. Contact us for more details.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
