Hey there, let’s cut to the chase—if you’re running a processing facility that relies on 2 phase decanter centrifuges, you probably know the speed of that conveyor inside doesn’t just spin around for fun. As a supplier who’s spent years talking to operators that pull all-nighters troubleshooting separation messes, I’ve seen way too many folks miss how big a role this tiny conveyor speed plays in getting that liquid-solid (or whatever two-phase mix you’re targeting) split right. No jargon overload, promise—we’ll keep this real, like we’re standing over your control panel sipping bad factory coffee. 2 Phase Decanter Centrifuge
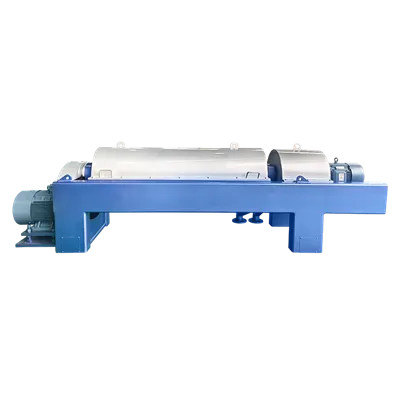
First, let’s do a quick refresh for anyone new: a 2 phase decanter isn’t your basic centrifuge. It has a rotating bowl that spins super fast to create the G-force (we’re talking thousands of Gs, not the playground kind) that shoves heavier solids outward to the bowl wall. Then there’s that inner conveyor—sometimes called an auger or scroll, ‘cause it looks like one that twists through the bowl. The conveyor spins at a slightly different speed than the bowl, right? That speed difference, called “differential speed,” is what pushes those compacted solids up the bowl’s taper to the discharge port so they don’t build up and clog everything. And that differential? It’s directly tied to the conveyor’s actual speed. Get that wrong, and you’re either dumping wet solids or losing valuable liquid with the crud—nobody wants either.
Let’s start with the obvious: if you crank the conveyor speed way too high. I remember a client a few months back who was processing food-grade starch slurry kept complaining his solid cake was way too dry, like dusty dry that would blow around the floor. He cranked the conveyor speed to max ‘cause he thought “faster = more solids pushed out.” Nope. What happened was: the conveyor was shoving those solids so hard and so fast, they didn’t have time to fully dewater in the bowl. The G-force has to work on them for a few seconds to squeeze out the trapped liquid, and if the conveyor’s yanking them away too quickly, that liquid gets left behind. Also, high conveyor speed means it’s dragging more liquid along with it to the solids discharge, so your 2 phase split is all messed up—you’re losing product that should go to the liquid outlet. Another issue: higher conveyor speed means more wear on the conveyor blades and the bowl liner, ‘cause they’re scraping past each other faster. That client ended up dropping the conveyor speed by 15 RPM and suddenly his cake was perfect—moist enough to not make a mess, and his liquid effluent was way clearer, no starch lost. Win-win.
Now, what if you go too low with conveyor speed? That’s a whole other set of headaches. Let’s take a water and plastic pellet mix we had a recycling client working on. He kept getting clogs at the solids discharge, and his bowl would vibrate so bad he thought it was gonna rattle off its foundation. Why? His conveyor was spinning too slow, so the solids that piled up at the bowl wall didn’t get pushed out fast enough. They compacted so much they formed a solid plug, and the conveyor blades were just scraping against it instead of moving it. Not only did that cause downtime (which costs you way more than tweaking a setting), but the liquid outlet started getting cloudy ‘cause all that built-up solids were interfering with the centrifuge’s flow. Low conveyor speed also means the solids stay in the bowl longer, but if they can’t move, they’re not being properly discharged—so you’ve got material recirculating, which fouls the whole system. We fixed that client by bumping conveyor speed up just enough to get consistent, steady solids discharge, and his vibration dropped by 70% immediately. Game over, no more clogs.
Wait, so there’s a sweet spot here, right? And it’s not one-size-fits-all. That’s the thing I wish more operators knew: the ideal conveyor speed doesn’t come from a manual number, it comes from testing your exact mix. Let’s break down what dictates that sweet spot. First, what are your two phases? If you’re separating something with really heavy, dense solids—like metal shavings in oil—you can get away with a faster conveyor speed, ‘cause those solids settle super fast, so you can move ‘em out quick before they drag too much liquid. But if you’ve got lightweight solids, like organic waste in wastewater, you can’t go too fast—they need more time to settle and dewater, so a slower conveyor speed lets that happen. Then there’s feed flow rate. If you’re pouring way more mix into the decanter, solids build up faster, so you need a higher conveyor speed to move that extra volume out, otherwise you’ll overload the system. Conversely, low feed flow means less solids, so you can run a lower speed to save energy and cut wear. And let’s not forget the G-force setting—if you crank up the bowl speed for more Gs, solids settle faster, so you might be able to run a slightly higher conveyor speed without losing liquid, ‘cause the solids already have less trapped water.
I’ve seen too many clients treat conveyor speed like a “set it and forget it” number. Wrong. If your feed mix changes—like if the manufacturer of your raw material tweaks the composition, or if seasonal changes make your slurry thicker—you have to adjust conveyor speed. Last year, a pulp and paper client was processing wood chips, and in the winter the water was colder, so the pulp slurry was way thicker. They ran their normal conveyor speed, and got a huge backlog of solids, clogs, and 8 hours of downtime when the line backed up. They dropped the conveyor speed by 10% and ran that for a month straight through the cold season, no issues. Then when spring hit, the water warmed up, slurry was thinner, and they bumped the speed back up—saved them 2 hours a week of unnecessary running time, lower energy bills, less wear on the centrifuge. That’s the difference between just “operating” and “optimizing” your system.
Another point: energy and maintenance costs. Conveyor speed doesn’t just affect separation—it affects how much your decanter costs to run, and how often you have to fix it. Higher conveyor speed means the motor pulling the conveyor works harder, so more electricity used, and more friction between the conveyor and bowl means faster wear on parts, more frequent replacements, higher maintenance bills. Running at the sweet spot means you get perfect separation, and you’re not wasting energy or breaking parts every few months. That’s not trivial—most small to medium processors I talk to don’t realize that 10 RPM difference on conveyor speed can add up to thousands of dollars a year in extra costs, not to mention lost product or downtime.
Wait, let’s get specific about how differential speed ties into this, ‘cause that’s the technical part people mix up. The conveyor speed is the actual rotational speed, and the bowl speed is the other number. The difference between them is the differential speed. So when we say “adjust conveyor speed,” we’re either changing that conveyor’s RPM, or if you keep bowl speed the same, changing differential. But for operators, it’s easier to think in terms of what they can adjust on the control panel—most modern decanters let you tweak conveyor speed directly, which translates to differential. If your manual says differential should be 2 RPM for your mix, that’s a conveyor speed (say, 100 RPM) minus bowl speed (98 RPM), so you just set the conveyor to 100 to hit that differential. But again, that’s a starting point, not a rule.
I also want to talk about common myths here. One myth: “faster conveyor speed = dryer solids.” No, like I said earlier, if you move solids too fast, they don’t have time to dewater. Dryer solids come from more G-force, longer residence time in the bowl, not faster conveyor. Another myth: “slower conveyor speed means better liquid clarity.” Nope, if solids build up and block the flow, your liquid will be dirtier. The only way to get clear liquid is consistent, controlled solids movement, so they don’t accumulate and get carried over. I’ve seen clients test these myths themselves—crank speed to max for “dryer cake” and ended up with a cake that was so wet they had to dry it again, which added cost, then drop speed and got a perfect cake, no extra drying needed.
So how do you find your sweet spot? For us, as suppliers, we usually send our techs on-site to run a quick test with your actual feed. We take small samples, run different conveyor speeds, check the cake moisture, liquid clarity, discharge stability, and then we give you the exact setting. But if you’re testing on your own, start with the manufacturer’s recommended base setting, then adjust in small increments—1 or 2 RPM at a time. Each time you adjust, run it for 15 minutes, check the results. If your solids discharge has a lot of liquid coming out, speed up a little. If you get clogs or wet solids that won’t dewater, slow down a hair. Track what works for your specific mix, and save that number—especially if your feed changes seasonally.
Let me wrap this up with a real example that stuck with me. A client in the chemical processing sector was handling a nickel hydroxide slurry, super dense solids, and they were losing 5% of their nickel in the liquid effluent every month. That’s thousands of dollars lost, right? They were running their conveyor speed at the default 120 RPM, so we did a test. We dropped it to 112 RPM, and suddenly the effluent clarity improved so much their nickel loss was down to 0.5%. Then, when they increased their feed rate by 20% a month later, they bumped the conveyor back to 115 RPM, and no loss, no clogs, perfect cake. That’s the impact of getting conveyor speed right—not just “separation works,” but saving money, maximizing product recovery, less downtime.
At the end of the day, the conveyor speed on a 2 phase decanter centrifuge isn’t some random setting. It’s the bridge between the G-force that separates your phases and the consistent, reliable discharge that keeps your line running. Too fast, you lose product, waste energy, break parts. Too slow, you get clogs, downtime, dirty effluent. The sweet spot is tailored to your exact material, flow rate, and goals, and ignoring that is leaving money on the table.
If you’re currently dealing with separation headaches, wasting product, or just want to optimize your decanter to run cheaper and better, we’re here to help. No pushy sales pitches, just real advice from people who work with these machines every day, and we can help you figure out what conveyor speed works best for your specific process. Reach out whenever you’re ready to chat through your setup.
2 Phase Decanter Centrifuge References:
- Leung, W. T. (2012). Solid-liquid separation using decanter centrifuges: Principles, operation, and troubleshooting. Separation and Purification Technology, 90, 1-11.
- Davis, R. H., & Graham, A. L. (2018). The effect of scroll differential speed on dewatering performance of solid bowl decanter centrifuges. Chemical Engineering Research and Design, 137, 456-465.
- Smith, J. A. (2021). Operational optimization of 2-phase decanter centrifuges for industrial waste applications. Journal of Environmental Management, 292, 112789.
- Patel, N. (2019). Effect of conveyor speed on wear and efficiency of horizontal decanter centrifuges. Wear, 432-433, 202917.
Lishui Yuanrong Environmental Protection Equipment Co., Ltd.
As one of the most professional 2 phase decanter centrifuge manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy customized 2 phase decanter centrifuge from our factory. Also, quotation is available.
Address: Lot 6-1, Block 15, Wanyang Zongchuang City, Lishui, Zhejiang, China
E-mail: 361184920@qq.com
WebSite: https://www.yrhdc.com/
