Hey there! If you’re anyone who relies on thermocouples for anything from industrial furnaces to food processing lines, you already know the drill: one tiny measurement slip-up can throw off an entire process, cost you hours of downtime, or even risk product quality. As a thermocouple supplier, I’ve seen so many folks shrug off “small” accuracy issues until they blow up into way bigger problems. So let’s cut the jargon and get real—here’s how to actually make your thermocouple measurements more accurate, not just guess at them. Thermocouples

First off, let’s start with the basics that a lot of people skip: right out the gate, thermocouples aren’t all created equal. You wouldn’t use a Type K thermocouple (the common nickel-chromium/nickel-aluminum one) for high-temperature vacuum work, right? I’ve had customers come to me with a $50 thermocouple meant for a 1200°C furnace trying to use it in a 1800°C kiln—total mismatch, and their readings were off by hundreds of degrees before they even got it out of the box. So step one: pick the right type for your temp range, environment, and application. If you’re dealing with corrosive gases, go with a mineral-insulated (MI) thermocouple with stainless steel or Inconel sheath, not a bare wire that’ll eat through in a week. Need precision for lab work? Type S (platinum-rhodium/platinum) is your guy, even if it’s pricier than Type K. Cheap thermocouples might seem like a steal, but they’re often made with off-spec wire that has inconsistent alloy levels—That’s accuracy lost before you even install it.
Next up, installation is way more important than most people think. I can’t tell you how many times I’ve visited a customer’s site (okay, “visited” is code for “fielded a panicked call at 2 a.m.”) where someone just jammed the thermocouple into a hole they drilled, no attention to how it’s touching the wrong parts. First rule: thermocouples measure their junction, not the sheath. If the hot junction (the end where the two wires meet) isn’t fully immersed in the medium you’re measuring, you’re getting a reading of whatever it’s touching instead. For example, if you’re measuring liquid in a tank, stick the junction at least 3x the sheath diameter below the surface—shorter than that and you’ll get cold air seeping in, skewing the reading. And never let the junction touch the tank wall if the wall is a different temp than the liquid; a customer once had their oven’s temp readings 200°F off because the thermocouple was pressed against the cold oven door instead of the hot air inside. Also, avoid bending the wires near the junction—micro-cracks from rough handling can cause tiny voltage fluctuations that add up to big errors. Pro tip: use a thermowell when you can. It protects the junction from corrosion, vibration, and physical damage, but make sure the thermowell fits tight so there’s no air gap between the sheath and the well. Air is an insulator, so that gap will make your reading lag and be inaccurate.
Then there’s cold junction compensation (CJC)—this is the secret sauce a lot of DIYers and small operations sleep on. Thermocouples work on the Seebeck effect: the voltage difference between two different wires depends on the temp difference between the hot junction (where you’re measuring) and the cold junction (where the wires connect to your meter/controller). If the cold junction isn’t at a known, stable temp, your readings will be wrong. Old school folks used to use an ice bath for cold junction compensation, but that’s a pain for most sites now. Most modern controllers have built-in CJC, but double-check it! A lot of cheap controllers skip proper temperature sensors for CJC, so they’re off by 5–10°C just from being mounted near a hot motor. If you’re using a handheld meter, make sure it has accurate CJC or you can manually input the cold junction temp. I once had a bakery client whose oven’s bread was coming out underbaked because their controller’s CJC was sitting right next to a 350°F conveyor, so it thought the cold junction was 100°F hotter than it actually was—their thermocouple was reading 50°F lower than real temp, no wonder the loaves weren’t rising.
Calibration isn’t a “set it and forget it” thing, either. I see customers calibrate their thermocouples once when they install them and never touch ’em again, but that’s a mistake. Even the best thermocouples drift over time, especially in harsh environments. How often should you calibrate? Depends on the application: food processing might need it every 6 months, a high-temperature furnace with corrosive vapors might need it every 3, a quiet lab setup can go a year. Don’t just send it to some random lab—look for a calibration service that uses traceable standards, meaning their equipment is calibrated against national metrology standards (like NIST in the US). And if you’re in a pinch, a quick field check works too: for lower temps, use boiling water (100°C at sea level, adjust for altitude) to test if the thermocouple reads correctly. For higher temps, a melting point standard—like lead at 327°C or aluminum at 660°C—can give you a rough idea. And if your thermocouple is off by more than 1–2% of its full range, replace it or have it recalibrated. I’ve had customers try to “tweak” their controller to fix a drift, but that just creates a band-aid error that gets worse over time.
Wire and connector quality matter more than you’d guess. The extension wires (the long cables that run from the thermocouple to your controller) aren’t just regular copper wires—they have to match the thermocouple type. If you use copper wires for a Type K thermocouple, you’ll create extra junctions that add voltage errors. Cheap extension wires have inconsistent insulation, too; if they’re exposed to high temps or chemicals, the insulation can break down, leading to short circuits or signal loss. Also, don’t leave extra wire coiled up near hot equipment—if the extension wire gets too hot, it acts like another thermocouple, throwing off the signal. And connectors! A loose or corroded connector is a huge source of error. I’ve seen readings jump 50°F just because a connector had a little rust on the pins. Use gold-plated connectors if you’re working in humid or corrosive environments—they don’t corrode as easy as tin-plated ones. Also, make sure the connector is rated for your temp range; a plastic connector meant for room temp will melt if it’s near a 500°C line.
Wait, let’s talk about signal noise, too. A lot of industrial sites have big motors, inverters, or welders that create electromagnetic interference (EMI). That noise can mess with the tiny voltage signal a thermocouple produces (it’s only millivolts, super sensitive). How to fix it? Run extension wires away from power cables—at least 12 inches apart, if you can. Don’t run them in the same conduit. Twist the extension wires together (twisted pair) to cancel out EMI, and use shielded cable if you’re in a really noisy area. Ground the shield at one end only—grounding at both ends creates a ground loop that adds noise, trust me on this. I had a customer in a automotive plant whose weld shop was messing up their thermocouple readings on a paint oven; we switched to shielded twisted pair and ran it in its own conduit, and their readings stabilized immediately, no more random spikes.
Oh, and let’s not skip maintenance checks. Even if you install a great thermocouple, it’ll degrade over time. Inspect it regularly for sheath cracks, wire damage, or corrosion. If you’re using a thermowell, pull it out every few months and clean any buildup on it—scale or residue on the well insulates it, so your thermocouple can’t sense the actual temp. I once had a cement plant client whose thermowell was caked in kiln dust, so the thermocouple reading was 100°C lower than the actual kiln temp, and they didn’t notice until we inspected the unit. Cleaning the thermowell fixed it right up. Also, if you’re using a disposable thermocouple (like for single-use batch processes), don’t reuse them—they get damaged during use, and the accuracy drops fast.
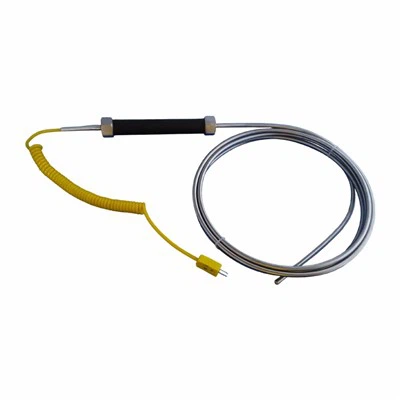
Now, I know a lot of this sounds like a lot, but it’s all stuff that adds up to way better accuracy without breaking the bank. You don’t need a $1000 thermocouple; you just need the right one installed right, calibrated regularly, and cared for properly. If you’re tired of guesswork in your temperature measurements, or if you’re not sure what type of thermocouple is right for your application, reach out. I’m here to help you pick the right product, give you tips on installation and calibration, and make sure you get the accurate readings you need to keep your process running smoothly. Don’t let small accuracy issues turn into big headaches—let’s chat about your needs.
Digital Temperature Controller References
- Measurement Specialties. (2022). Thermocouple Selection and Installation Guide.
- National Institute of Standards and Technology (NIST). (2021). Temperature Measurement Standards for Thermocouples.
- Omega Engineering. (2023). Cold Junction Compensation Best Practices.
- ISA (International Society of Automation). (2020). Industrial Temperature Measurement Calibration Procedures.
Jiangsu Zhaolong Electric Co., Ltd.
We’re well-known as one of the leading thermocouples manufacturers and suppliers in China, featured by quality products and low price. Please feel free to buy customized thermocouples made in China here from our factory. Contact us for more details.
Address: No. 80, Zhangguo Chang’an Road, Dainan Town, Xinghua City, Jiangsu Province
E-mail: 180193845@qq.com
WebSite: https://www.cnzhaolong.com/
